Map the inspection faces
Mark the required regions on a drawing and show how the casting arrives. Identify recesses, edges and shadowed areas that the proposed view cannot see; these remain open requirements until a suitable method is established.
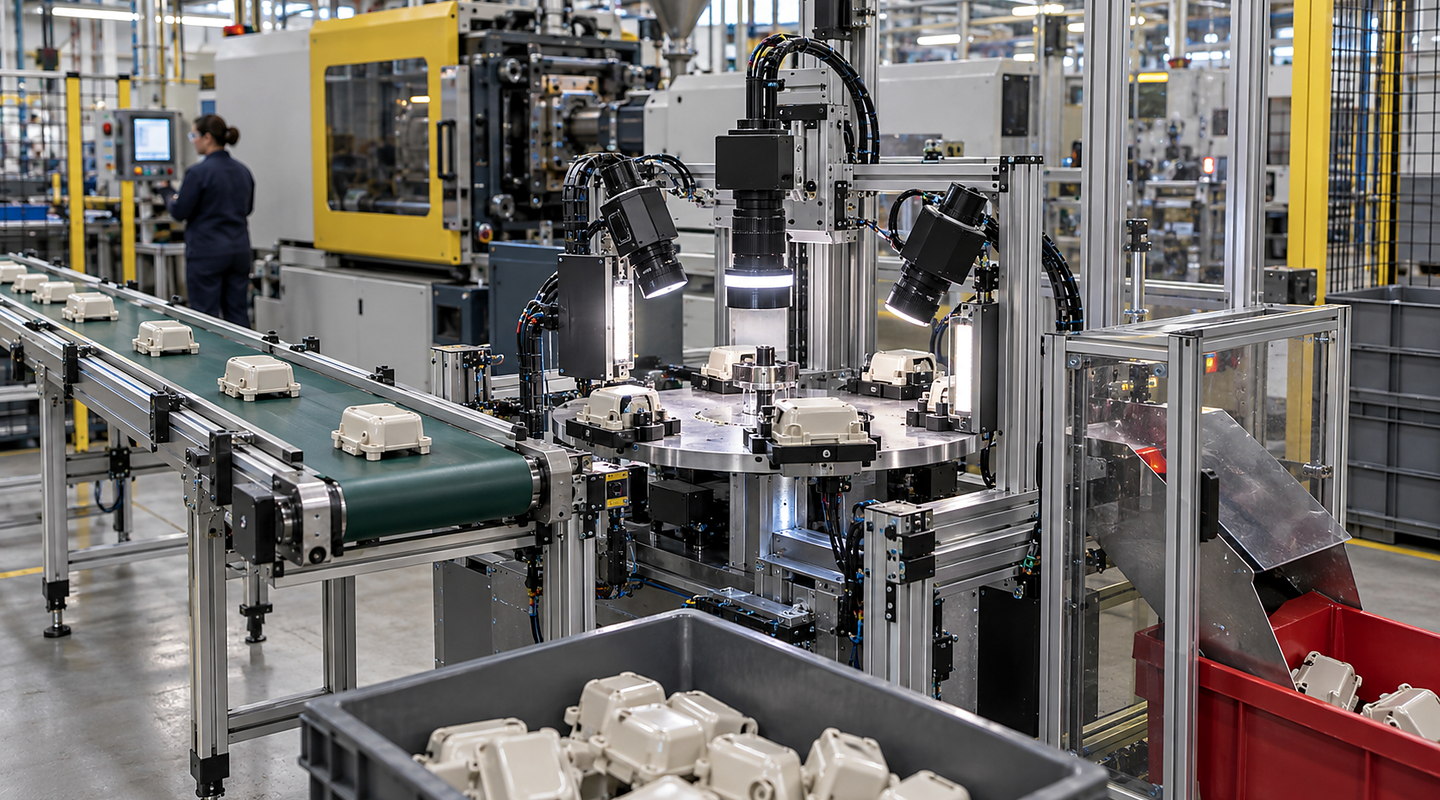
Define which casting defects are visible and must be distinguished from acceptable variation. Use representative good, bad and marginal parts to assess presentation, lighting and inspection criteria; a visible check must not be confused with a hidden or functional test.
Speak directly with Oxford Vision Systems about visible casting-defect inspection.
Photographs illustrate general machine-vision inspection. Casting suitability must be assessed using representative castings, defined visible defects and the actual presentation.
Define each defect and whether it is exposed to the proposed camera views. Supply castings showing acceptable surface variation, marginal defects and the smallest feature of concern. Record any hidden or functional requirement separately so that an optical inspection trial is not mistaken for evidence about the whole casting.


A casting-inspection brief should name the visible decision, the surface to be viewed and the variation that remains acceptable on a good part.
Mark the required regions on a drawing and show how the casting arrives. Identify recesses, edges and shadowed areas that the proposed view cannot see; these remain open requirements until a suitable method is established.
Use labelled examples of the visible feature rather than a general instruction to find bad castings. State its permitted location, size or appearance and who approves the boundary between acceptable and unacceptable.
Supply good parts from normal batches and finishing conditions. Differences in texture, colour or residue must be represented so the trial does not confuse ordinary production variation with a defect.
Define the datum, orientation and support points. Trial the least repeatable presentation expected on the line, including normal casting tolerances, rather than relying on a carefully positioned laboratory sample.
Compare images of good and defective regions with the proposed lighting and camera access. More complex software cannot establish a property that the optical arrangement has not made observable.
Specify how a failed or unreadable result reaches the correct reject, rework or review position. Include missing parts, unexpected variants and interrupted cycles in the control sequence.
Read the in-line casting inspection guide to turn the required surface checks into an assessable production sequence.
The right choice changes with visible defect or measurement definition for visible casting-defect inspection, good, bad and marginal sample range, your line layout and required results.
The trial record should identify each inspected region, sample condition and demonstrated defect. Also record excluded faces and uncertain results so the production team knows what has and has not been assessed.
After adjusting the inspection, test further representative parts without treating the development samples as the entire acceptance set. Review missed defects and rejected good parts separately.
A visible surface check is not evidence about hidden internal features or functional performance. List those requirements alongside the camera brief and assign them to the appropriate inspection or test process.
Use the casting inspection cameras specification checklist to prepare the application, then agree the acceptance checks and production records before comparing proposals.
Your final solution for visible casting-defect inspection must reflect the law, current standards and site-specific risks that apply to your installation.